Our QC and QA team upholds high standards through systematic inspections, audits and compliance checks, using the following equipment:
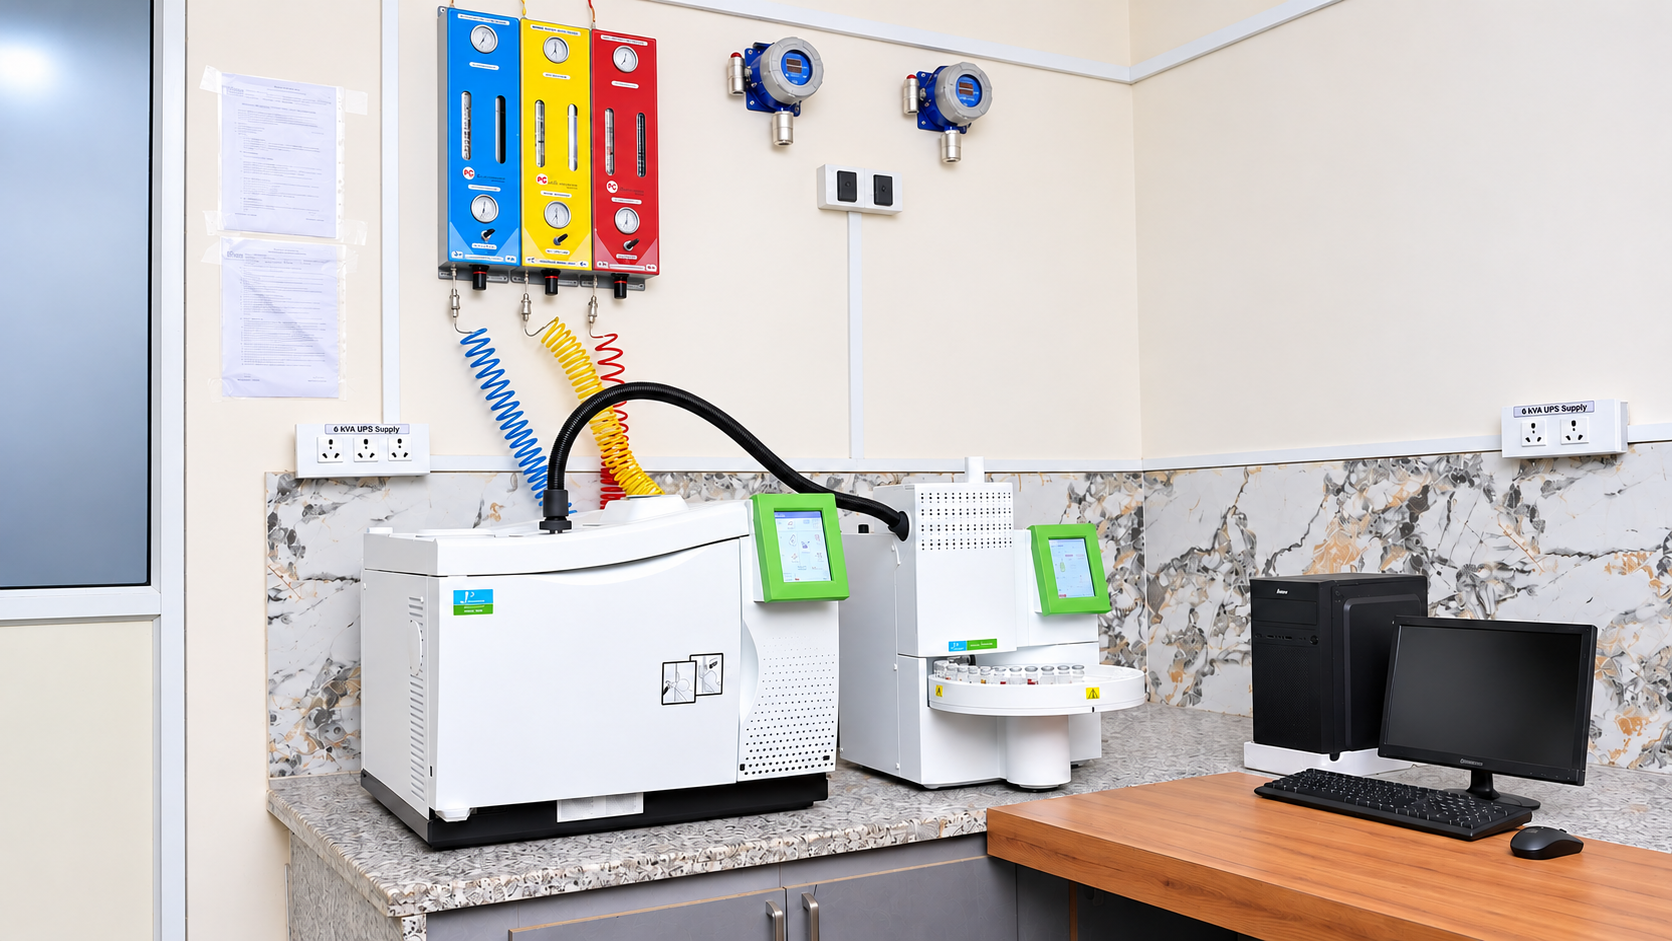
Analyzes residual solvents in laminates
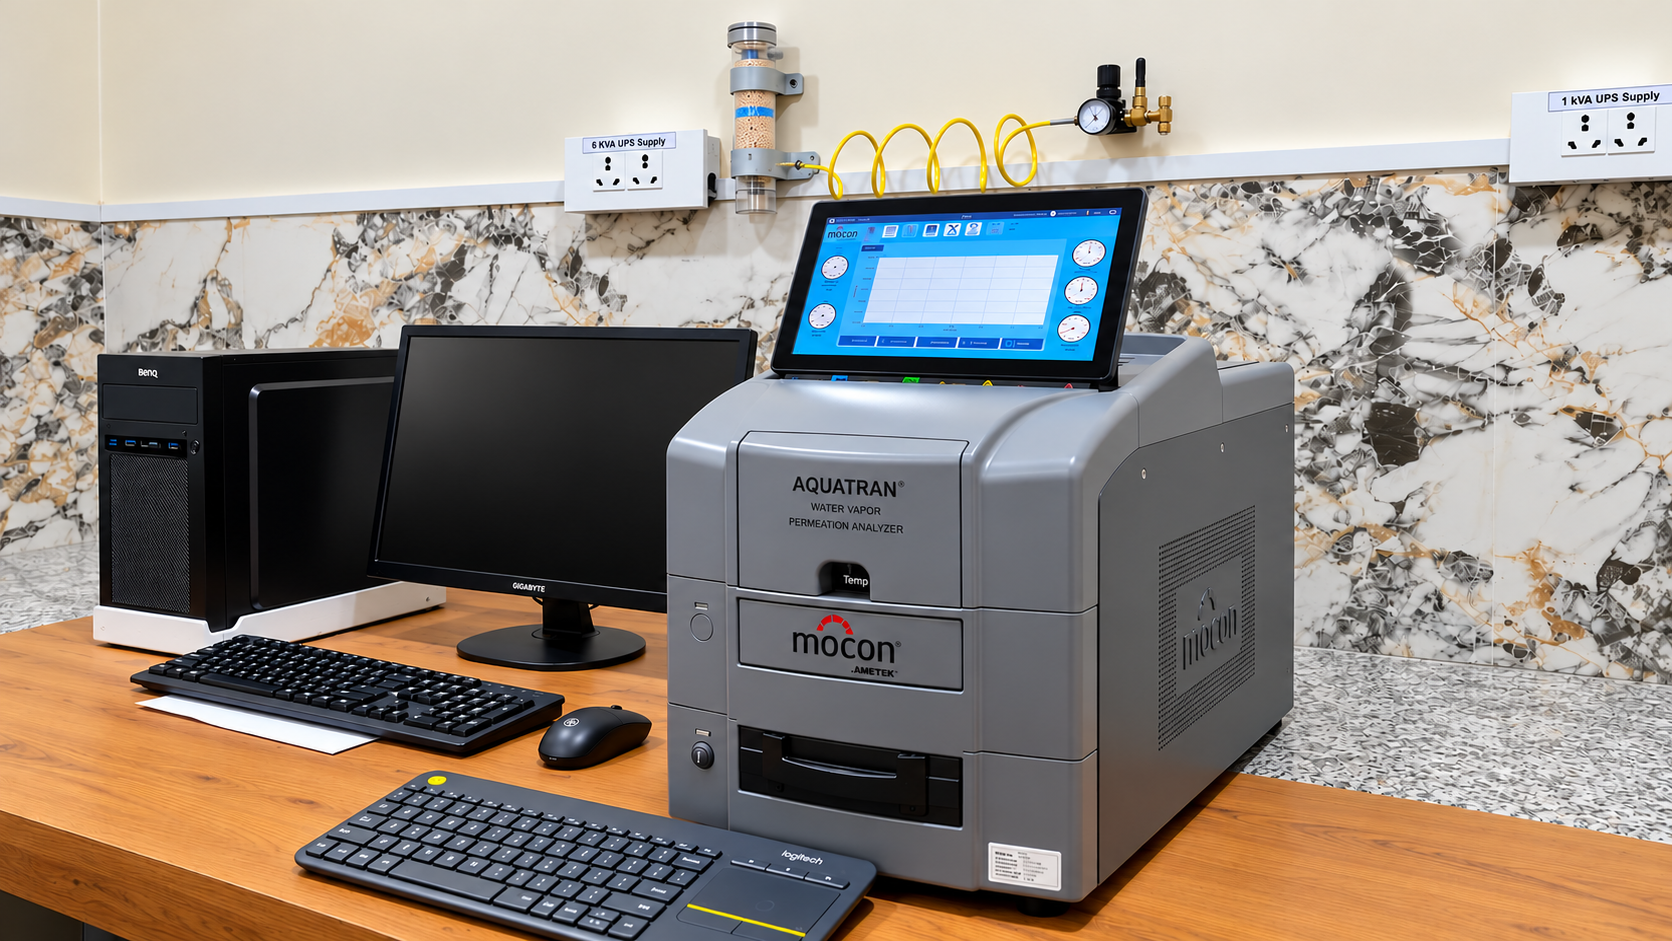
Assesses barrier properties and shelf life
Measures oxygen permeability in packaging materials.
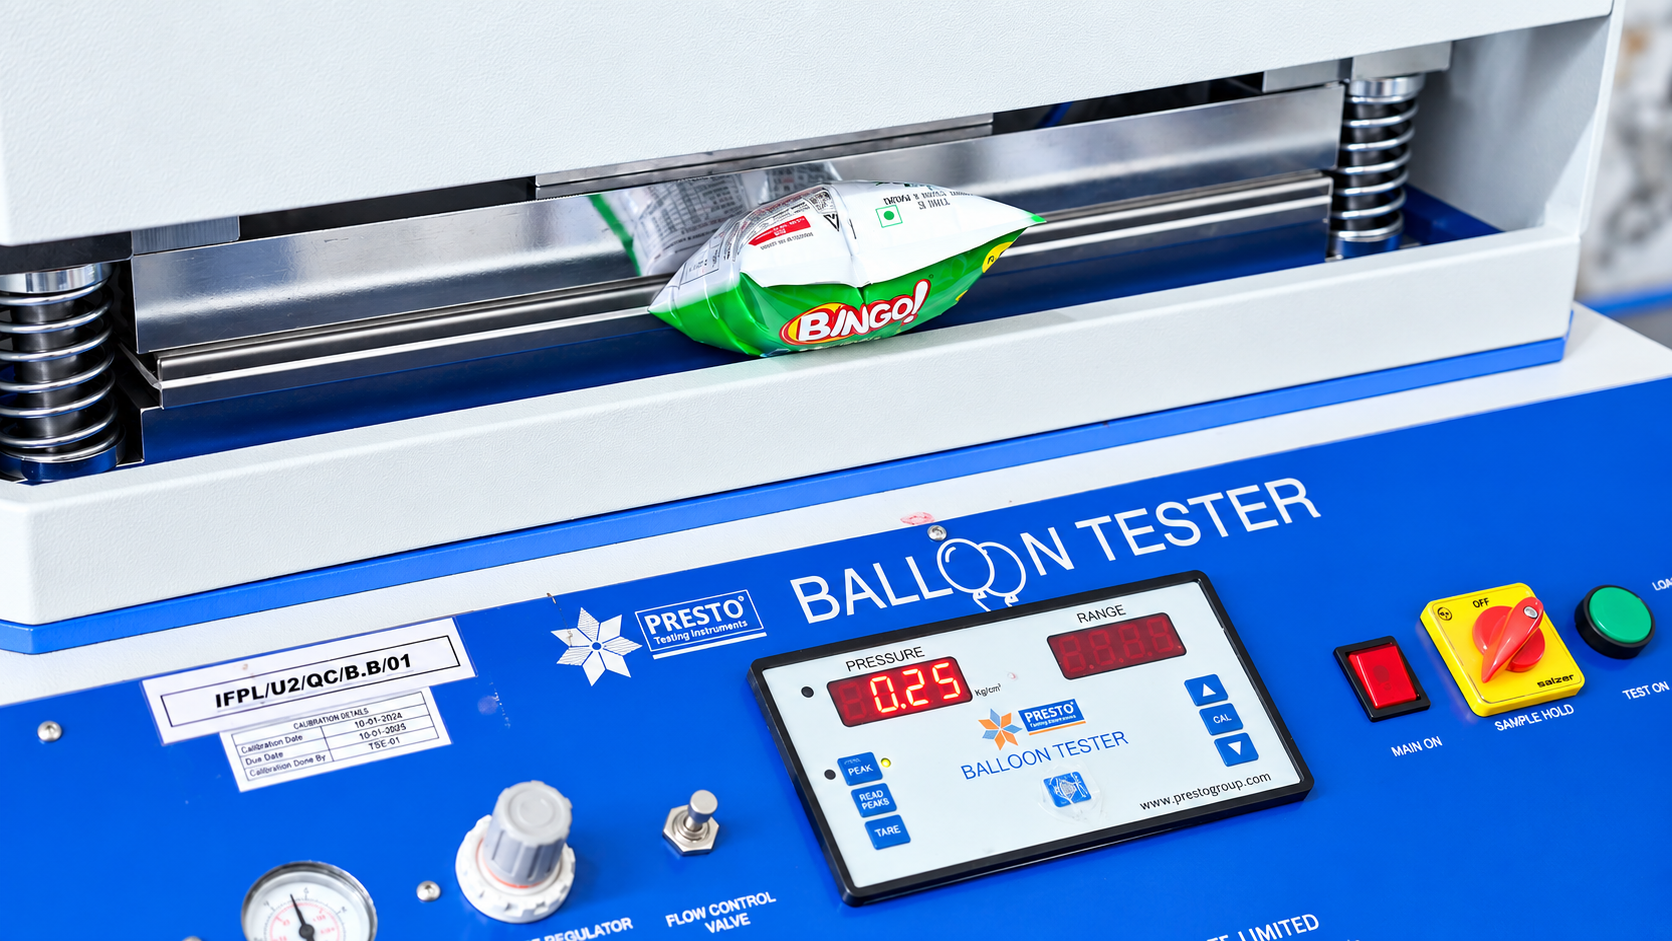
Evaluates seal integrity under pressure
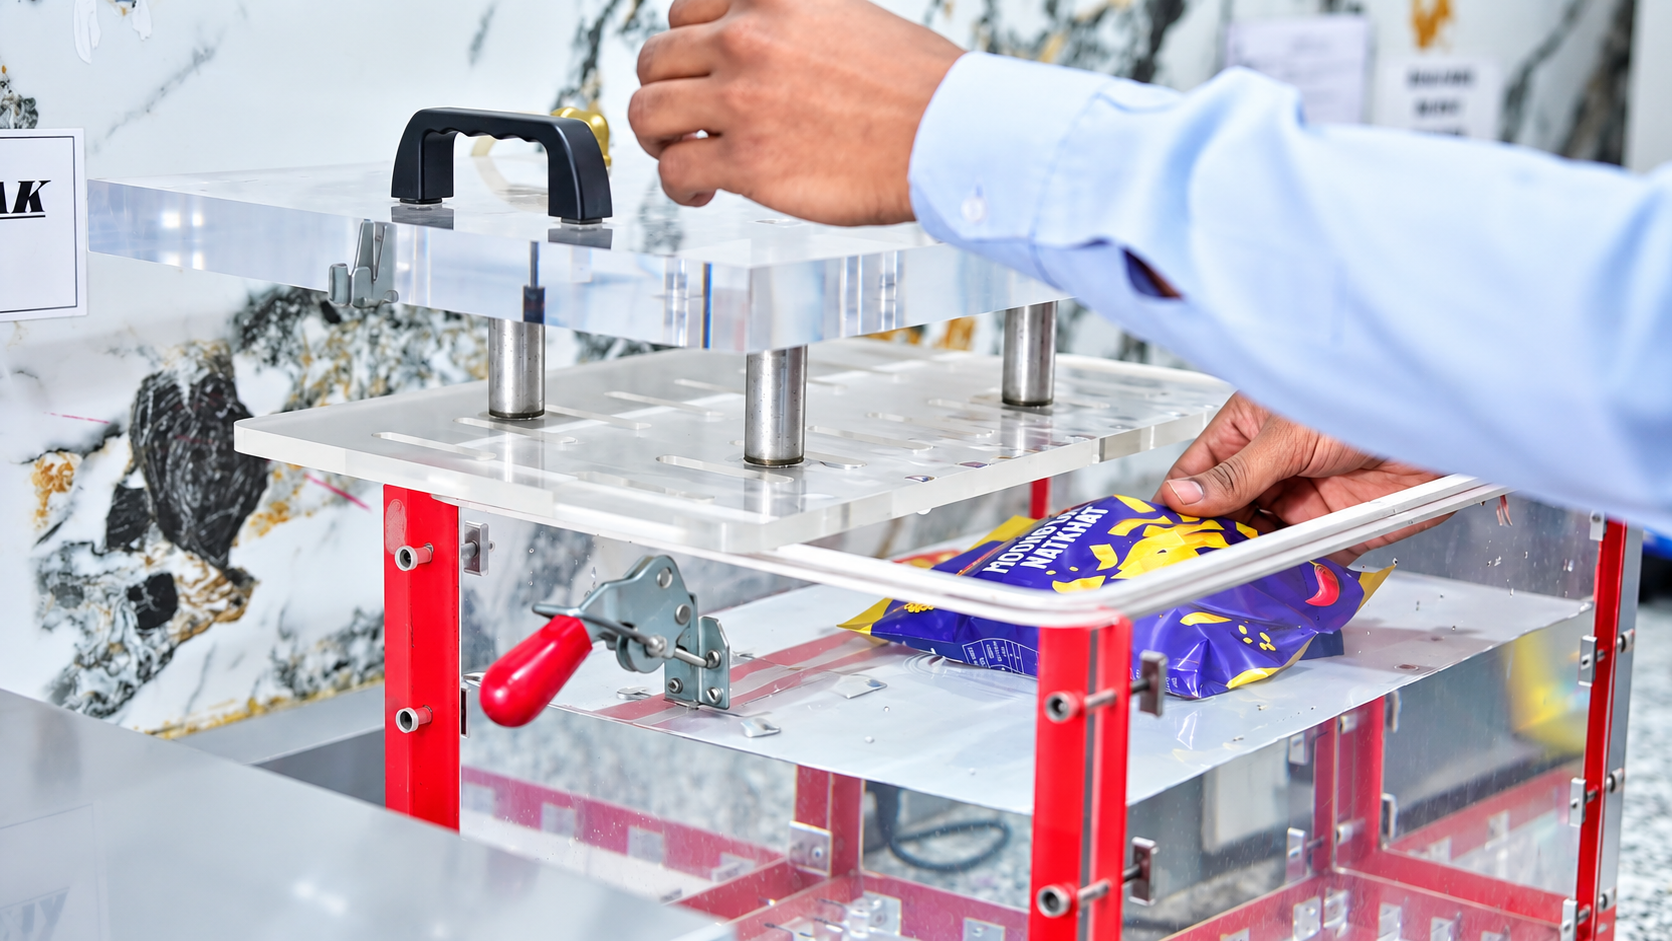
Ensures reliability of vacuum seals
Tests tensile strength and elongation
Measures friction properties of packaging films
Tests impact resistance of films
Ensures accurate, consistent colour reproduction
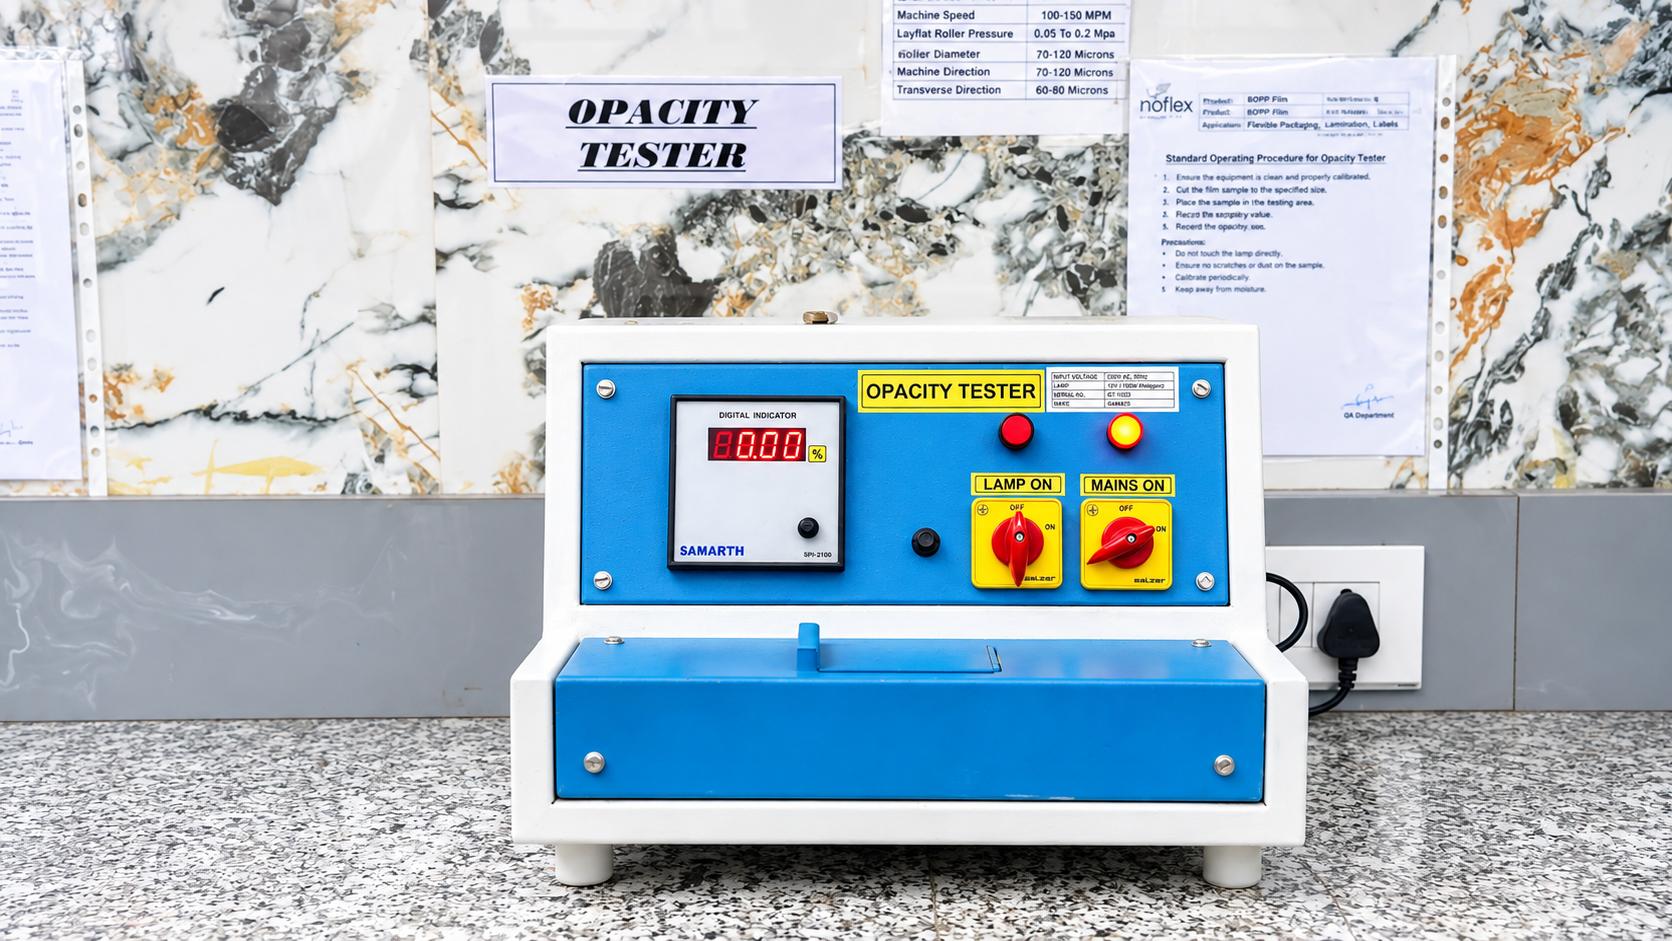
Measures opacity and light-blocking properties
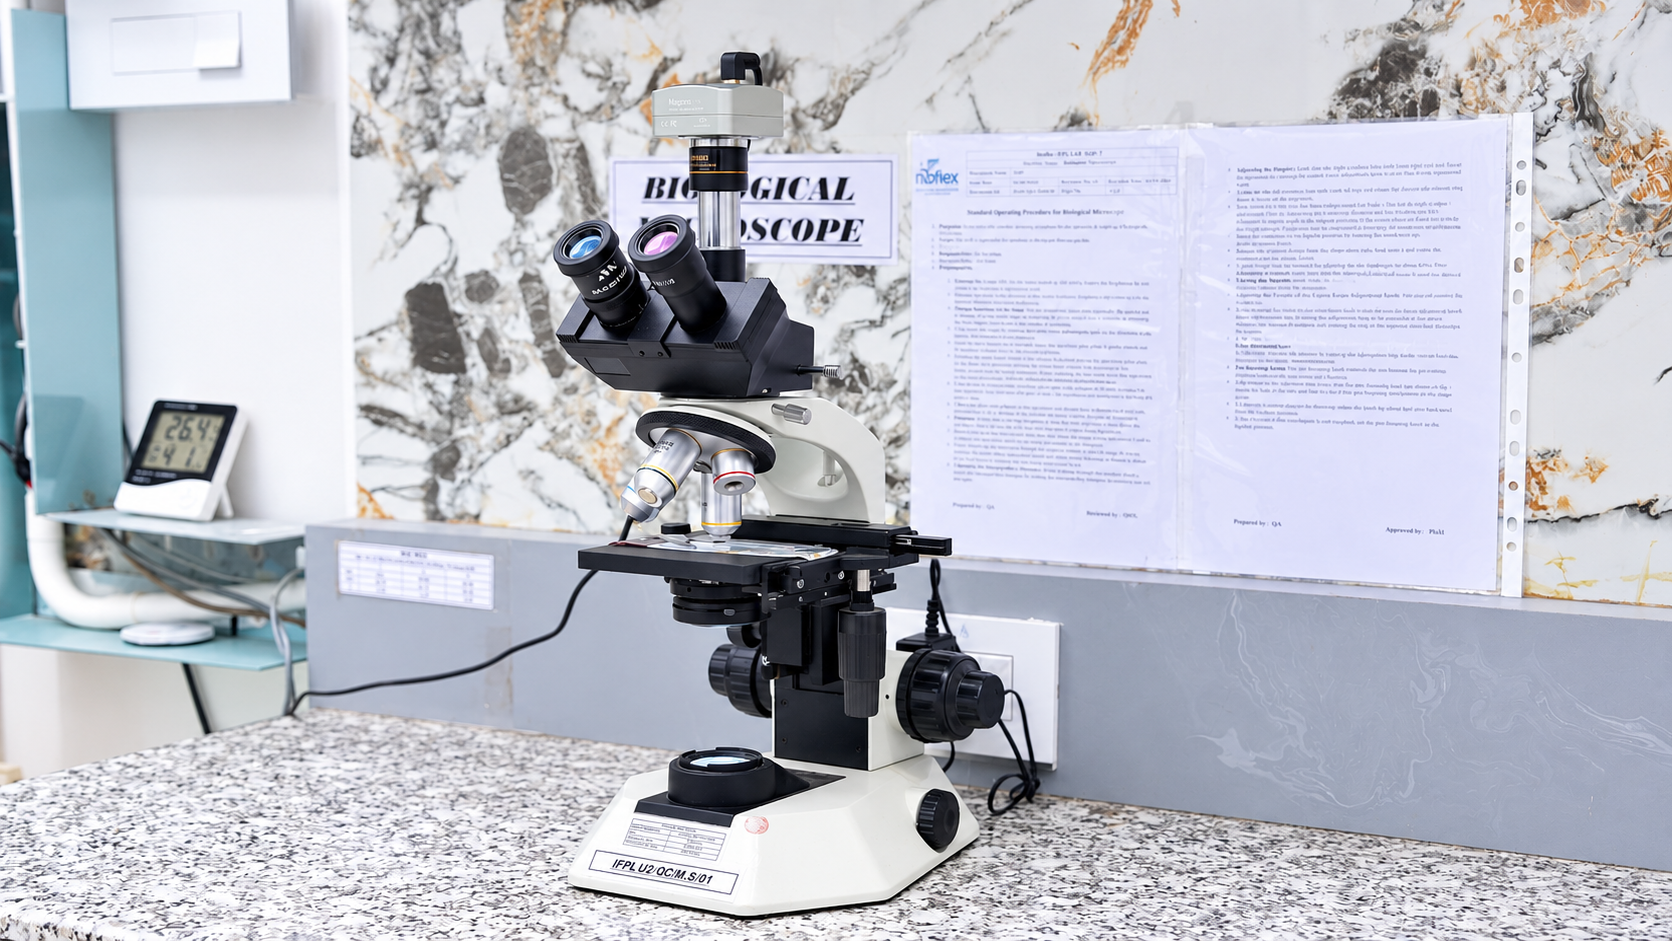
Used to inspect material quality and microscopic defects.
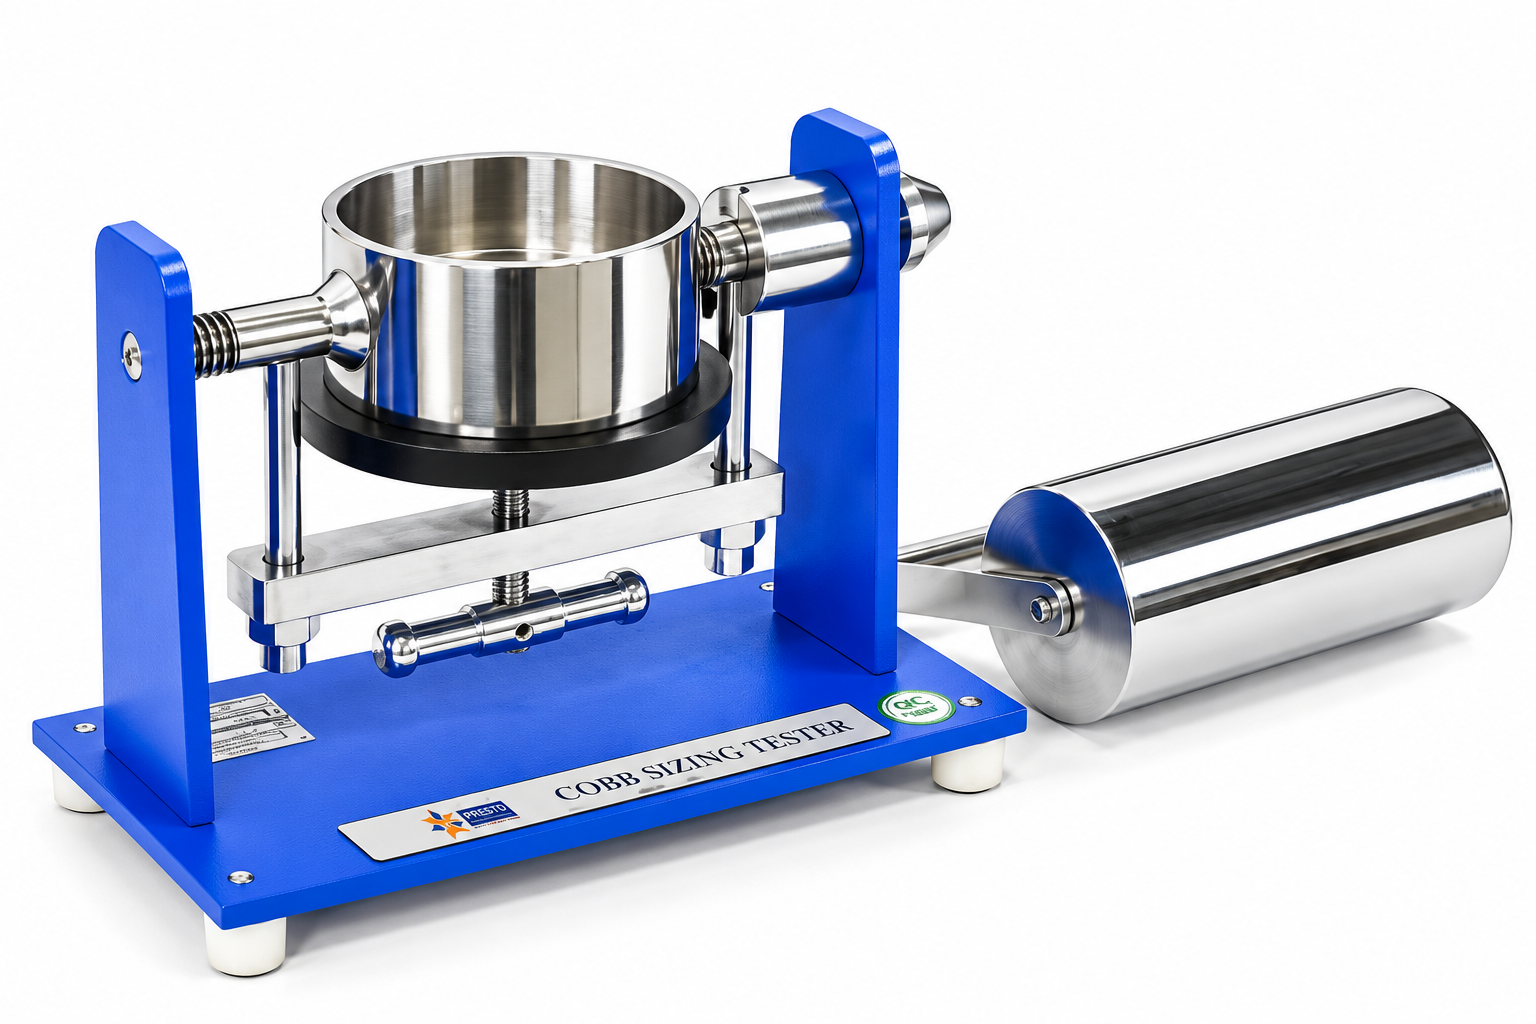
Measures water absorption of paper and packaging materials.